











by Dr David Sutter, Aquafeed Expert, FoR Aquafeed Consultancy, Germany
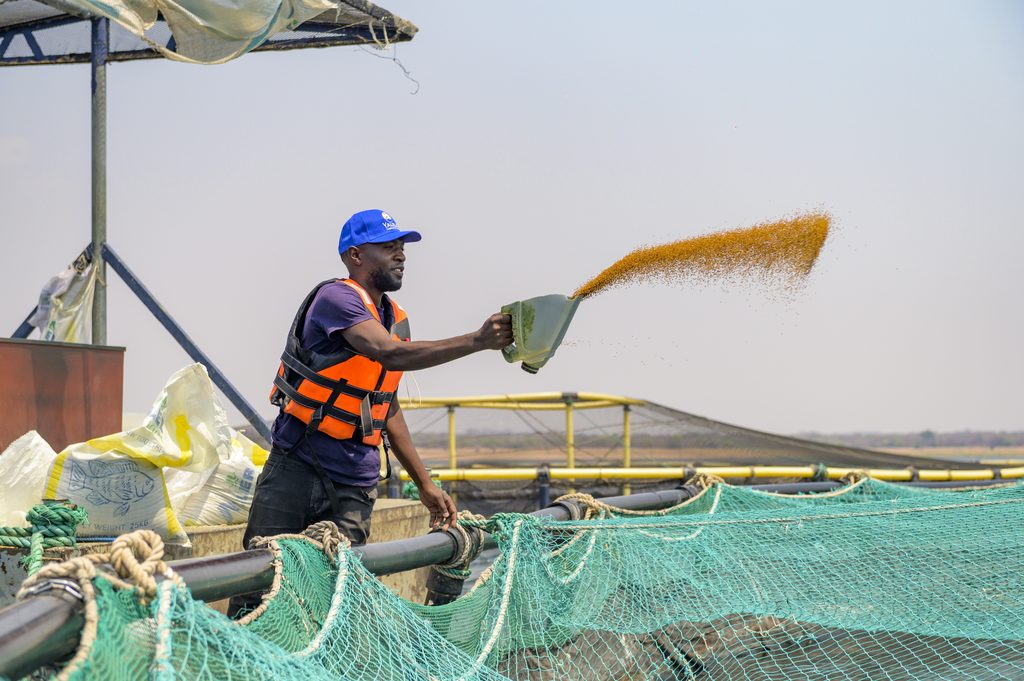
Zambia’s aquaculture sector has expanded rapidly in recent years. Cage farming on Lake Kariba has contributed to this growth, with Yalelo among the producers scaling up tilapia production. The mill was commissioned in 2017 and now operates as Kamimbi Aqua Feed, supporting a reliable supply of high-quality feed near Yalelo’s large-scale fish production site in Siavonga.
Good fish feed must provide all necessary nutrients but nutritional specifications alone are not sufficient. A homogeneous pellet structure, appropriate pellet size, consistent floatability, water stability, durability and cost efficiency all need to be considered. Meeting these requirements can become more difficult when a feed mill operates in a remote location within a landlocked country. Aquafeed production in such locations is often affected by the availability and consistency of raw materials. In Zambia, raw material supply depends largely on road transport over long distances, while imported materials may need to cross several borders.
The structure of the agricultural sector also shapes raw material sourcing, with supply dispersed across many farming operations of different sizes. Aggregators therefore play an important role in consolidating sufficient volumes and connecting producers with large-scale buyers such as feed mills. This supply structure places particular importance on raw material specifications, quality control and reliable supplier relationships.
Spare parts for technical equipment present a related logistical consideration. International deliveries can take several months, requiring critical spare parts to be kept on site and maintenance activities to be carefully planned. Smooth and stable production is especially important, both to maintain feed supply and to minimise unnecessary wear, breakdowns and rework. Maintaining and further improving this operational reliability is therefore an ongoing focus at Kamimbi Aqua Feed.
Linking formulation and processing
So, where does feed formulation come into play? Its contribution goes beyond providing the required nutrients. Feed formulation and raw material selection also affect mash functionality, processing efficiency and the physical properties of the final feed.
Fish feeds must meet several physical requirements. Pellets should be uniform and appropriately sized for the target fish species and life stage to support efficient feed intake and reduce losses. In tilapia production, high and consistent buoyancy is generally desirable. Pellets should also have a homogeneous pore structure that supports post-extrusion liquid application while maintaining water stability. At the same time, sufficient durability and elasticity are needed to reduce breakage and dust formation during storage and transport.
Emphasis is often placed on grinding, mixing and setting the correct extruder parameters. These factors are fundamental, but feed formulation can help maintain suitable processing conditions. The desired pellet quality is therefore the result of the interaction between the feed formula, the process settings and the technical capacity of the mill.
Formulating for mash functionality
This makes it useful to consider the technological properties of the formula and of the individual raw materials used. Rather than establishing minimum inclusion levels for individual raw materials solely on the basis of their assumed nutritional or functional contribution, it is often preferable to establish formulation targets at the feed-mash level. Such targets consider the contribution of all raw materials in the formula. This increases flexibility in raw material selection and can help control formulation costs.
Forcing a particular raw material into a formula narrows the available formulation space and may add cost unless its inclusion provides a clear nutritional or technological benefit. This does not mean that limits for individual raw materials should always be avoided. Ingredient-specific minima or maxima can be justified where the behaviour of a material cannot be described adequately by general nutrient or mash-level targets.
Coarse fibre provides one example. Depending on the equipment in use, a raw material with high levels of coarse fibre may affect grinding efficiency and the particle size distribution of the final mash. Different grains and bulk raw materials can therefore produce substantially different mash structures, even when their proximate compositions appear similar. Where this behaviour affects processing, a maximum inclusion level for the individual raw material may be appropriate.
The role of starch, fat and fibre
The same principle applies to other technologically relevant constituents, particularly starch and fat. Starches from different raw materials may produce different expansion behaviour and gel characteristics after gelatinisation. Relevant factors include the amylose-to-amylopectin ratio, starch granule size, starch concentration and the physical matrix in which the starch is present. It is therefore not sufficient to consider only the total starch content. It is also useful to ask in what form the starch is supplied, how concentrated it is and how much fibre or fat accompanies it.
Mash fat also influences processing. High fat levels can reduce the hydration and swelling of starch granules and thereby limit expansion. Where possible, starch and fat should therefore be controlled directly at the feed-mash level rather than indirectly through fixed minima and maxima for wheat, maize or other individual raw materials. A minimum wheat or maize inclusion, for example, may add unnecessary cost if the required starch level and processing functionality can be provided through other ingredients.
Fine-tuning pellet quality
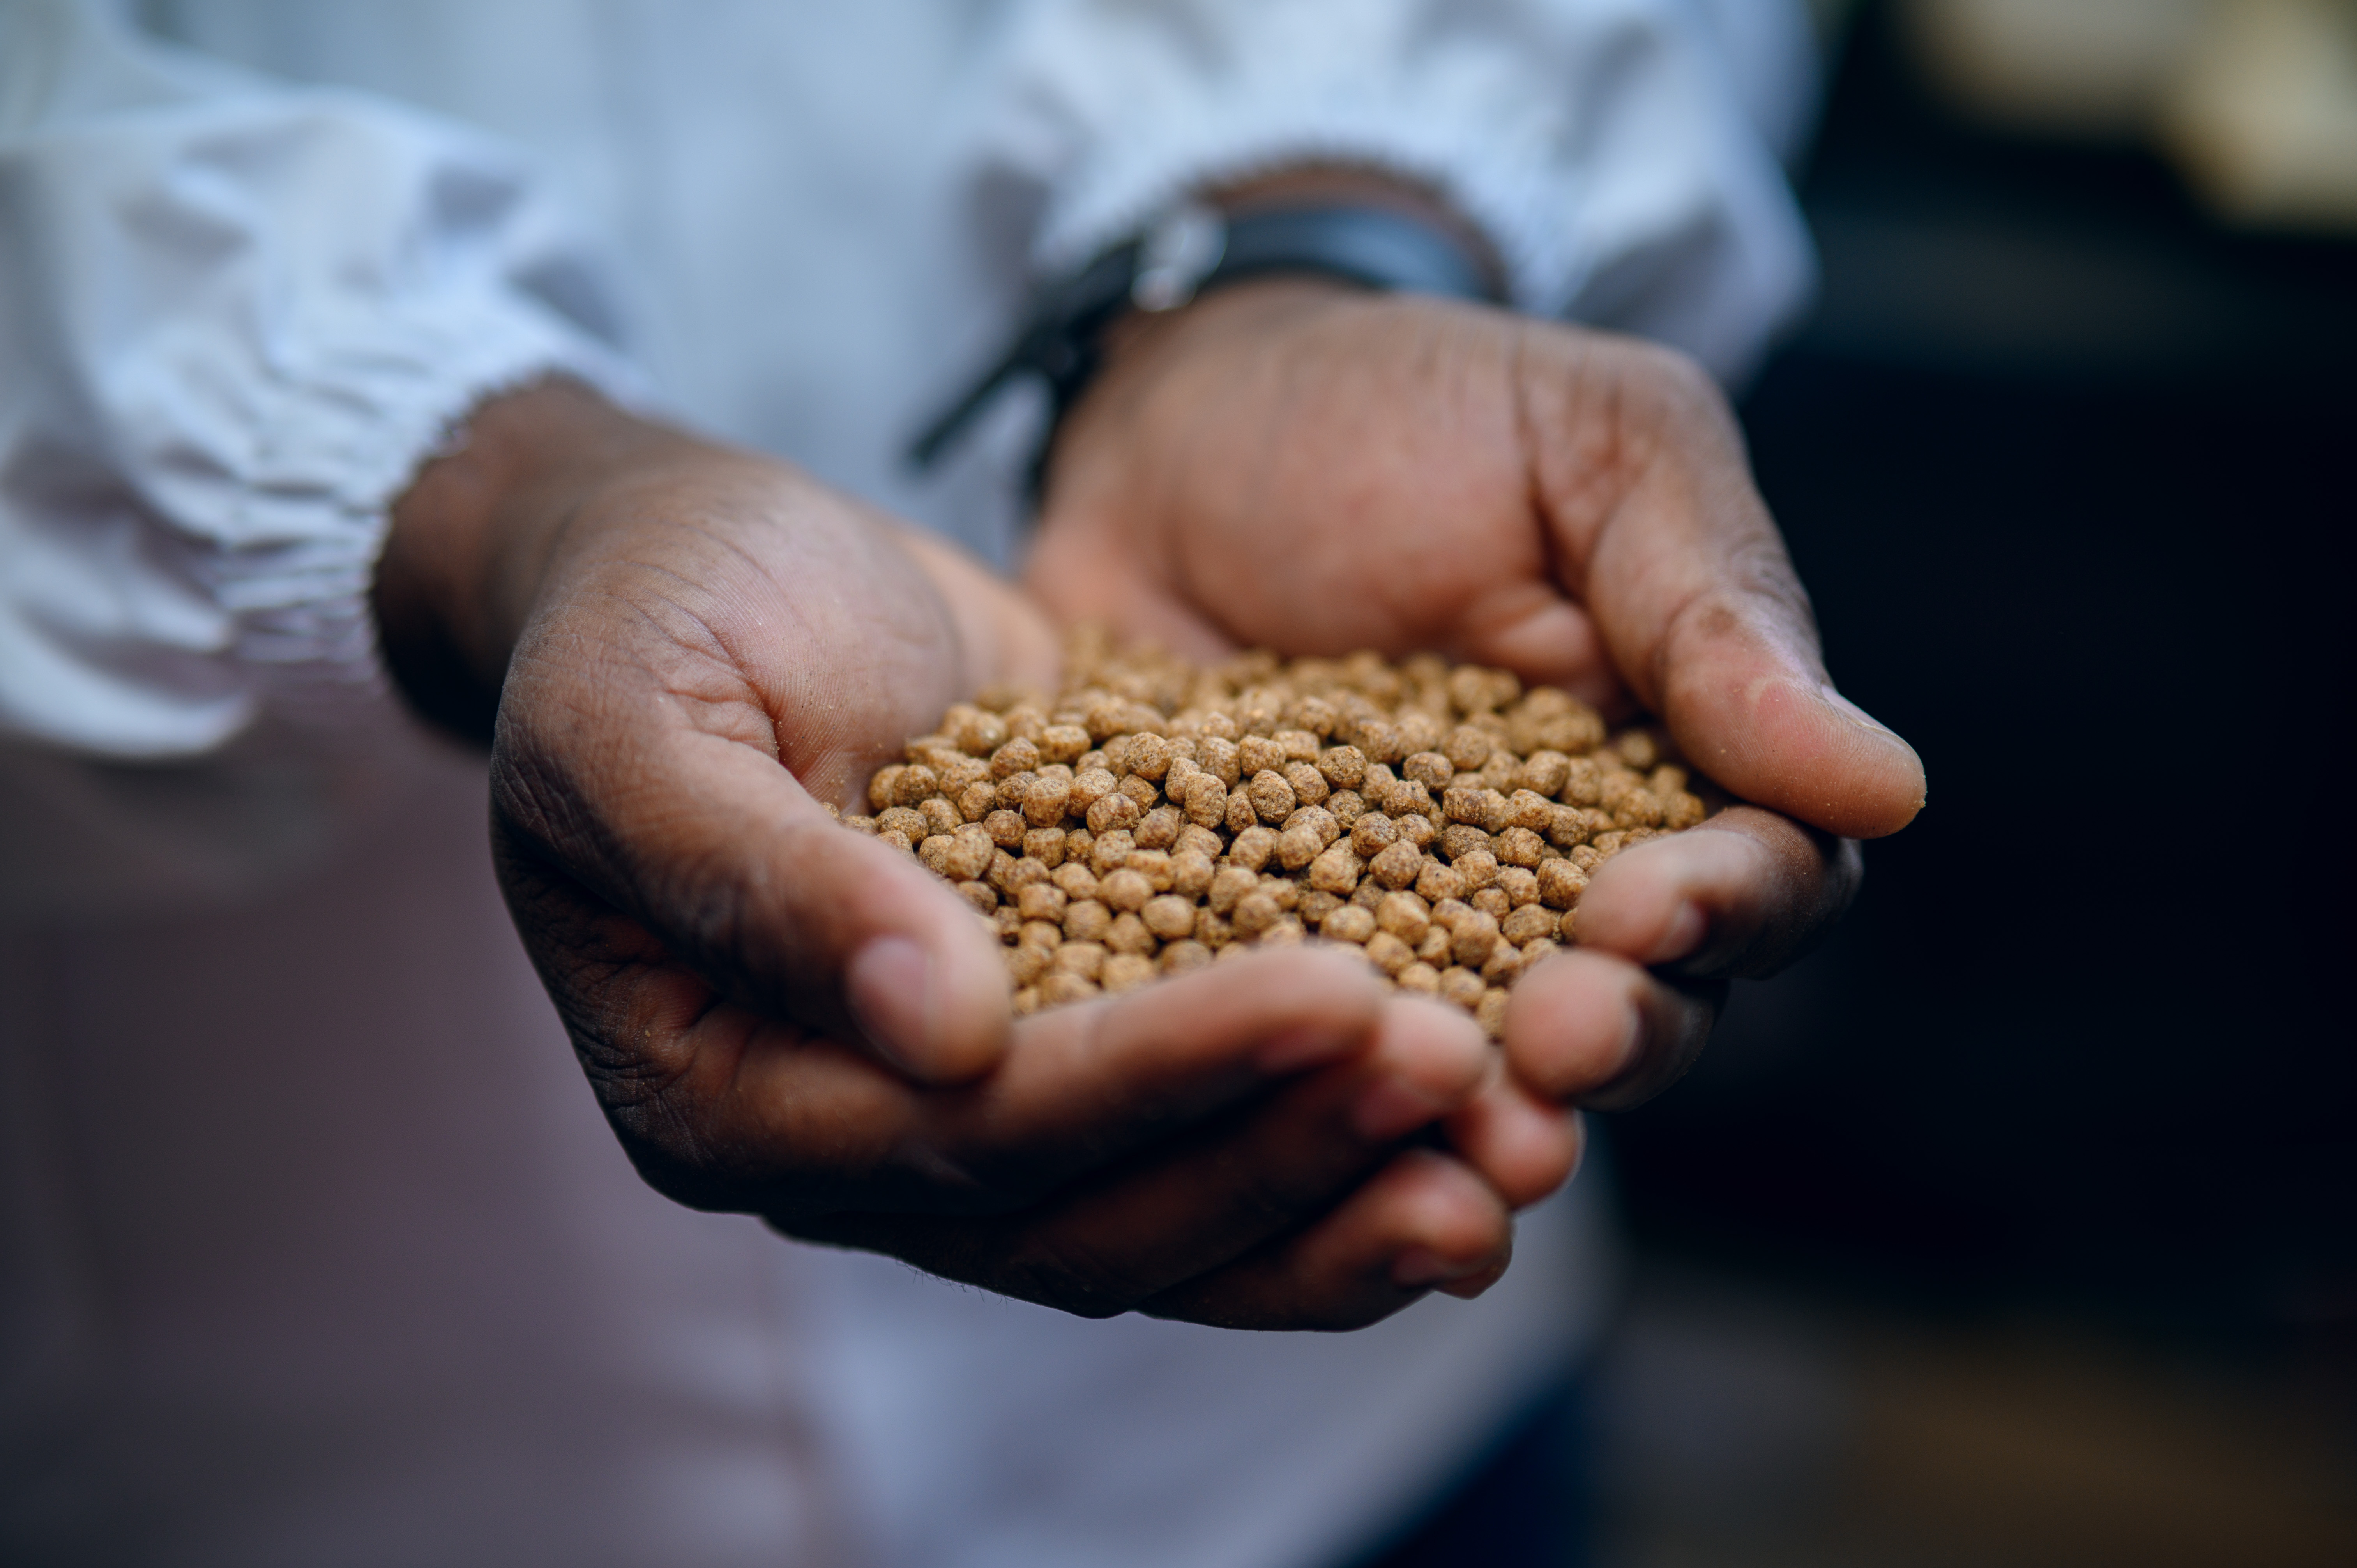
These considerations become particularly relevant in nutrient-dense formulas and feeds produced at small pellet diameters, where limited formulation space must be balanced against demanding physical specifications. At Kamimbi Aqua Feed, the fine-tuning of the physical properties of a 2 mm floating feed provided a practical example. Consistently high floatability, buoyancy and pellet uniformity were achieved by treating formulation and processing as closely connected parts of the development process.
This underlines that nutrient specifications alone do not determine how a formula will behave during production or whether the final feed will achieve the required physical properties. Similarly, successful processing requires careful consideration of the raw materials and, specifically, their functional properties. Hence, raw material costs provide only part of the economic picture. A formula that appears more expensive may still prove more cost-effective if it supports stable production, results in more consistent pellet quality, reduces the need for rework and increases hourly throughput. Therefore, the technological functionality of a raw material should be considered alongside nutritional value and cost.
This also illustrates why formulation and production cannot be considered independently. Optimal grinding, mixing and extrusion parameters remain essential, but their effectiveness depends partly on the characteristics of the mash entering the process. Close cooperation between production teams, formulators and nutritionists allows formulation decisions to reflect the capabilities and limitations of the mill. Equally, a practical understanding of raw material functionality helps formulators support process operators more effectively.
In operating environments such as that of Kamimbi Aqua Feed, raw material availability adds another dimension to the interaction between formulation and production. Where suitable materials are available, sourcing quality-approved raw materials locally or regionally can be advantageous. A sufficiently broad raw material portfolio provides formulators with alternatives when the supply of a particular bulk ingredient becomes constrained. This can help maintain greater consistency in feed composition and properties while improving procurement flexibility.
Making the most of local raw materials
Local sourcing generally shortens transport distances and reduces exposure to delays associated with multiple border crossings. In addition, the use of locally available crops and side-stream products allows farmers and other businesses in the agricultural value chain to participate in the growth of Zambia’s aquaculture sector. While these wider benefits are relevant, the primary focus is on raw material quality and the technological requirements of the feed mill. This may require raw material suppliers to provide more detailed analytical information beyond basic certificates of analysis indicating only crude protein and moisture.
In short, feed formulation is more than a means of meeting nutritional specifications. In an operating environment such as that of Kamimbi Aqua Feed, it also links raw material availability, processing efficiency and the physical quality of the final feed. Nutritional value remains fundamental, but formulators also need to understand the broader technological functionality of the raw materials used. Accounting for this functionality can help provide process operators with a mash that performs consistently during production. This helps ensure that the feed leaving the mill meets both its nutritional and physical quality objectives.